Running out of the right consumable mid-job is more frustrating than a bad weld. The rod in your hand decides penetration depth, slag behavior, and whether the joint holds under stress — so matching electrode type to metal, thickness, and process matters before you strike an arc. This guide explains the main welding rod types, stick, TIG, aluminum brazing and hardfacing, and shows ten example rods on Amazon so you can stock your toolbox with the right one.
Use the quick-picks table below to jump straight to the rod that fits your process, or read through each section for specs and who each rod suits.
Quick Picks — Jump to the Right Rod
- Easiest stick rod for beginners (thin steel): WISUNO E6013 3/32
- Best stick rod for heavier repairs: WISUNO E6013 1/8
- Best structural stick electrode: WISUNO E7018
- Best TIG filler for mild steel: WeldingCity ER70S-6
- Best TIG filler for stainless: Convivium ER308L
- Best hardfacing electrode: Forney Supercote
- Best low-temp aluminum brazing (torch): VITASHYNX Aluminum
Welding Rod Types Compared
| Rod type | Process | Metal | Good to know |
|---|---|---|---|
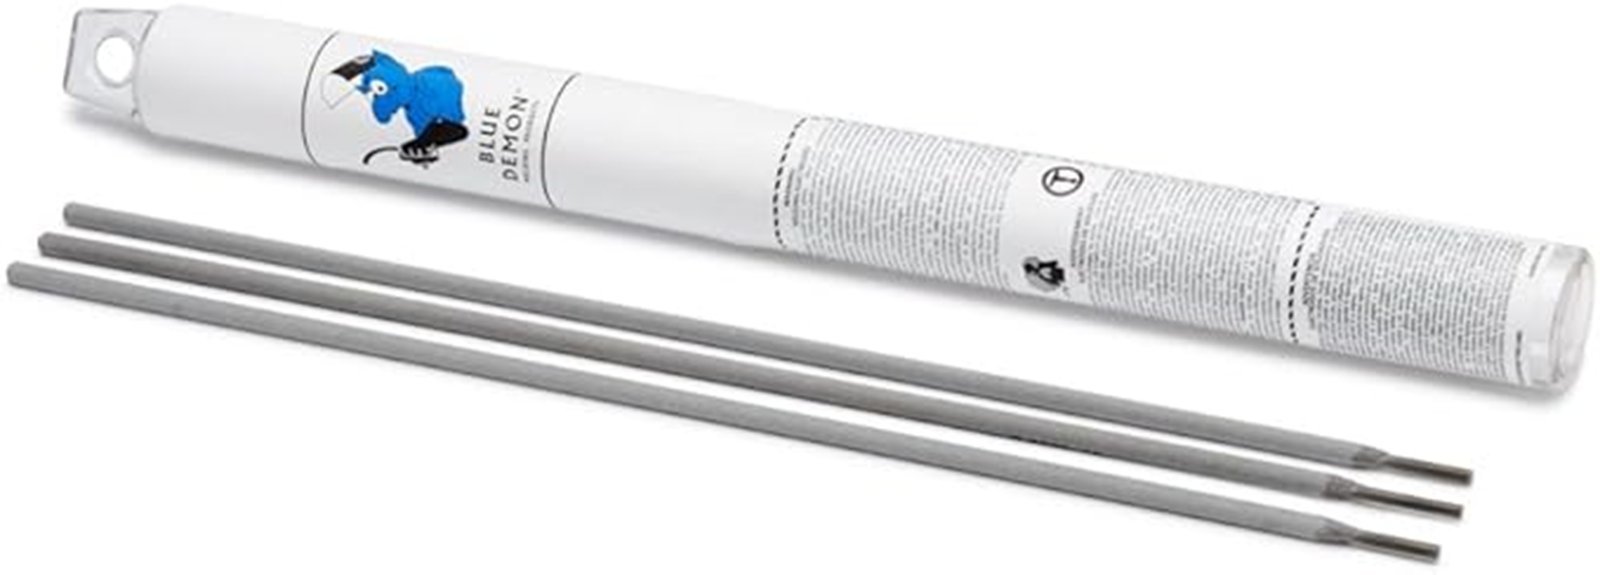
| E6013 | Stick (SMAW) | Mild steel | Easy to strike and runs on AC or DC; good for learning and light repairs |
| E7018 | Stick (SMAW) | Mild steel, structural work | Low-hydrogen; keep it dry; normally run on DC electrode positive |
| ER70S-6 | TIG (GTAW) | Mild steel | Bare filler rod; needs a TIG torch and shielding gas |
| ER308L | TIG (GTAW) | 300-series stainless | Low-carbon filler; use pure argon and clean metal |
| Aluminum brazing rods | Torch brazing | Thin aluminum | Not arc electrodes; need a high-output torch and clean metal |
| Hardfacing electrodes | Stick (SMAW) | Worn surfaces | Build up and protect worn parts; not for joining |
The 10 Rods by Type
| Category | Product |
|---|---|
| Best DIY Aluminum Brazing | SpaceWings Aluminum |
| Best Stick Rod for Light Fabrication | WISUNO E6013 3/32 |
| Best Stick Rod for Heavy Repairs | WISUNO E6013 1/8 |
| Best TIG Filler — Mild Steel | WeldingCity ER70S-6 |
| Best Flux-Core Aluminum Brazing Rod | AZB Flux Aluminum |
| Best Low-Temp Aluminum Brazing Pack | VITASHYNX Aluminum |
| Best Structural Stick Electrode | WISUNO E7018 |
| Best TIG Filler — Stainless Steel | Convivium ER308L |
| No-Flux Aluminum Brazing Rod | NIEFARG Aluminum |
| Best Hardfacing Electrode | Forney Supercote |
How to Pick From These Rods
Each rod below is grouped by the process it serves: stick electrodes (E6013, E7018), TIG filler rods (ER70S-6, ER308L), aluminum brazing rods and a hardfacing electrode. Match the type to your metal and machine first, then compare diameter and pack size. These notes reflect listing details and typical use, not bench testing. Confirm size, pack and price on the Amazon listing before you order.
1. SpaceWings Aluminum Brazing Rods — Best Budget DIY Aluminum Option

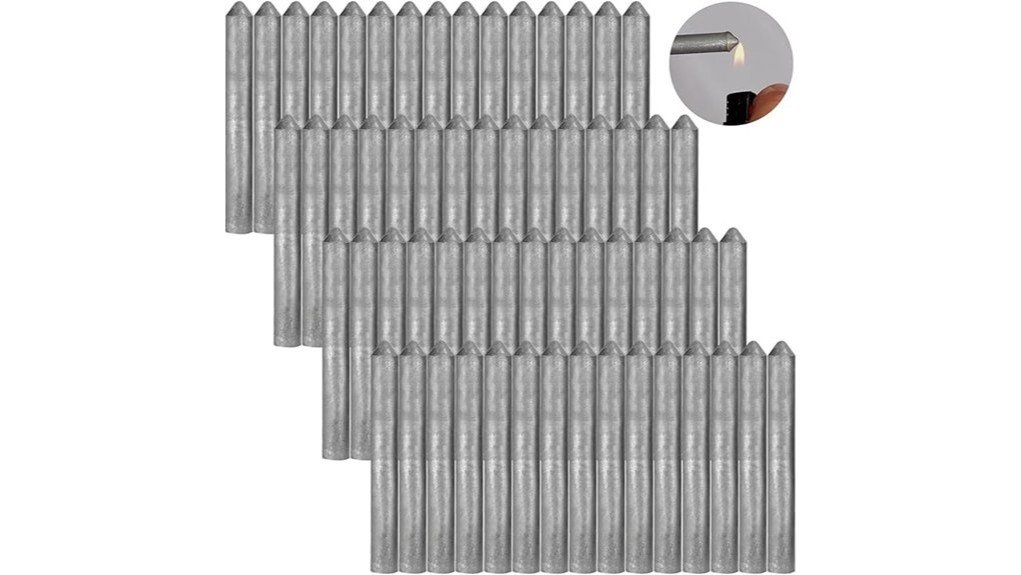
These rods are built for low-temperature aluminum brazing — patching thin sheet, HVAC fittings, and small fabrication work you can tackle without a full TIG setup. The 30-stick pack is compact and easy to store, and the solid aluminum composition is meant to flow into clean, properly heated joints when used with aluminum brazing flux.
They suit experienced DIYers and automotive technicians who already know how to prep aluminum and control torch heat. If you are still learning torch technique or working with thicker sections, you will likely find the margin for error too narrow here.
Key Benefits
- Low-temperature brazing for thin aluminum and alloys
- Compact 30-piece pack, easy to store and carry
- Solid aluminum construction for corrosion resistance in finished joints
Who Should Skip This
- Beginners learning torch technique — margin for error is low
- Anyone working on thick aluminum sections (>3mm)
- Welders who do not have a dedicated aluminum brazing flux on hand
2. WISUNO E6013 3/32 — Best Stick Electrode for Light Fabrication

Reach for these when you need a dependable, easy-to-run stick electrode. They strike readily, maintain a forgiving arc, and lay consistent beads on mild steel — which makes them a natural fit for hobbyists, learners, and anyone doing farm repairs or maintenance tasks with a compact inverter welder.
The 3/32″ diameter suits thinner plate and lighter-gauge work. If you move between repair jobs and don’t want to fuss with setup, these are a solid everyday rod to keep in the cabinet.
Key Benefits
- Easy to strike and maintain arc — ideal for beginners
- Works with small inverter and 110–220V welders
- Consistent bead quality for general repairs and light fabrication
Who Should Skip This
- Welders needing structural strength — step up to E7018 for load-bearing joints
- Anyone welding thicker plate (>3/16″) where 3/32″ diameter limits deposition
3. WISUNO E6013 1/8 — Best Stick Electrode for Heavier Repairs

Same forgiving E6013 chemistry as the 3/32″ version, stepped up to 1/8″ for more deposition on moderate-thickness mild steel. You get the same easy striking and steady arc, but with slightly better penetration suited to thicker plate, farm equipment repairs, and basic construction touch-ups.
Both inverter and conventional machines handle these well, so you can rotate between jobs without changing consumables. Packaging can allow moisture in, so inspect rods before use and re-seal the box after each session.
Key Benefits
- Easy striking and steady arc on moderate-thickness mild steel
- Compatible with AC and DC welders
- Step up in deposition from the 3/32″ version for heavier plate
Who Should Skip This
- Anyone needing structural-grade welds — E7018 is the right call there
- Welders working very thin sheet — the 3/32″ version is easier to control
4. WeldingCity ER70S-6 — Best Budget TIG Filler for Mild Steel

If you TIG mild steel regularly, ER70S-6 is the standard filler you reach for — and this 5 lb box from WeldingCity is a budget option. The 36″ rod length and multiple diameter choices suit bench work and larger assemblies equally well, and the rods respond predictably to standard argon or argon/CO2 shielding.
Keep them dry and you have a dependable go-to for color-matched welds, routine fabrication, and repair tasks where clean puddle control matters.
Key Benefits
- Smooth arc and consistent bead control across diameters
- Multiple diameter options in the same purchase
- Good colorization and predictable weld quality — important for visible work
- 5 lb pack offers better cost per pound than small retail packs
Who Should Skip This
- Stick welders — ER70S-6 is a TIG filler and requires a TIG machine and shielding gas
- Anyone welding stainless or aluminum — wrong filler for those metals
5. AZB Flux Aluminum Rods — Best Flux-Core Aluminum Brazing Rod

These rods simplify small aluminum repairs by combining flux inside the wire so you skip carrying separate flux. They work for patching thin sheet, pontoons, and light fabrication when you can bring the metal up to temperature and keep surfaces completely clean. The 50-piece pack gives you enough material for multiple small jobs.
The catch is that these rods demand more heat than many people expect. A small butane torch will not cut it on most repairs. You need at least a high-output propane or MAPP torch, and in some cases oxy-acetylene, to get reliable bonding.
Key Benefits
- Built-in flux — no separate flux needed
- 50-piece pack suited to multiple small repairs
- Compact length for access in tight spots
Who Should Skip This
- Anyone using a small butane or low-output propane torch
- Welders expecting arc-weld-level bond strength from a brazing rod
- Beginners who haven’t yet developed torch heat control
6. VITASHYNX Aluminum — Best Low-Temp Brazing Pack

These low-melt brazing sticks are designed to speed up small aluminum repairs without a TIG rig. The built-in flux simplifies setup, the 572°F–752°F working range suits propane and MAPP torches, and the 60-piece pack keeps you stocked across multiple jobs. For thin panels, HVAC fittings, and portable repair work, they are a practical addition to a torch kit.
The approach here is sound and the specs are clearly stated, but verify your torch output and surface prep match before depending on these for a critical repair.
Key Benefits
- Low melting range suits propane and MAPP torches
- Built-in flux eliminates separate flux handling
- 60-piece quantity for repeated repairs
- Clear temperature rating (572°F–752°F) makes heat matching straightforward
Who Should Skip This
- Welders using stick machines — this is a torch brazing rod only
- Anyone needing structural repair strength on load-bearing aluminum
7. WISUNO E7018 — Best Structural Stick Electrode

When a joint needs to hold under load, E7018 is the standard step up from E6013. The low-hydrogen coating resists moisture absorption and reduces the risk of hydrogen-induced cracking — which matters for structural fabrication, equipment maintenance, and any weld that will face stress in service. These give you a steadier arc and deeper penetration than the E6013s in this roundup.
The key discipline with E7018: store them in a sealed rod oven or airtight container. Exposed rods can absorb moisture and produce porosity. If you know your storage is solid, these are a reliable workhorse.
Key Benefits
- Low-hydrogen coating reduces cracking risk on structural welds
- Deeper penetration than E6013 for load-bearing applications
- Compatible with AC and DC stick welders for field and shop use
Who Should Skip This
- Complete beginners — E6013 is more forgiving for learning stick technique
- Anyone without proper dry storage — E7018 rods exposed to moisture underperform
- Thin-plate work where E6013 gives better control
8. Convivium ER308L — Best TIG Filler for Stainless Steel

ER308L is the standard TIG filler for 304 stainless, and the low-carbon composition is specifically important: it reduces carbide precipitation near the weld zone, which is what gives 308L its edge on corrosion resistance compared with regular 308. These rods feed cleanly into the puddle and give you predictable puddle control — useful for thin-gauge work where heat management matters.
The 16″ length and 20-piece pack suit bench work and lower-volume projects well. As with all stainless TIG work, pure argon shielding and clean base metal are non-negotiable for a quality result.
Key Benefits
- Low-carbon ER308L composition — correct choice for 304 stainless
- Smooth feed and stable arc for clean, consistent beads
- 16″ length suits bench work without excessive rod waste
Who Should Skip This
- Stick welders — ER308L requires a TIG machine and argon gas
- Anyone welding 316 stainless — ER316L is the correct filler there
- High-volume production work where a larger pack makes more sense
9. NIEFARG Aluminum — No-Flux Aluminum Brazing Rod

These rods are aimed at quick torch aluminum repairs without a full TIG rig and without the need for separate flux. The slender sticks fit into tight joints, and the no-flux claim simplifies setup in theory. In practice, expect a narrow margin for error.
They can work for small, well-prepped, well-heated repairs. But the margin for error is narrow: bad results usually trace back to insufficient torch heat, surface contamination, or expecting performance closer to TIG or stick welding than brazing can deliver.
Key Benefits
- No separate flux required
- Thin sticks for tight joints and detail work
- Designed for aluminum and Al-Mg alloys
Who Should Skip This
- Beginners — low margin for error without experienced torch control
- Anyone expecting easy bonding on thicker aluminum
- Welders using low-output propane torches
10. Forney Supercote — Best Budget Hardfacing Electrode

Hardfacing electrodes occupy a niche the other rods in this roundup don’t touch — you use them to build up worn surfaces and apply a wear-resistant overlay rather than to join two pieces of metal. The Supercote lays down a hard, machinable layer suited to resurfacing anvils, rebuilding machine surfaces, and adding abrasion resistance to wear plates and agricultural equipment.
The arc runs smoothly and the slag lifts cleanly, which speeds cleanup after each pass. The finished weld metal forges and grinds well, so you can shape the repair to fit. For heavy-impact applications — hammer dies, rock crushers — you would want a tougher specialty alloy, but for common workshop and farm resurfacing this rod hits the right balance of performance and price.
Key Benefits
- Smooth arc and easy slag removal — faster cleanup between passes
- Good for moderate abrasion resistance and surface rebuilding
- Weld metal can be forged and ground for finished surfaces
Who Should Skip This
- Anyone needing impact-resistant hardfacing — this rod is for abrasion, not shock
- Beginners unfamiliar with multi-pass hardfacing technique
Full Comparison Table
| Product Name | Image | Rod Type | Material | Length | Best Application |
|---|---|---|---|---|---|
| SpaceWings Aluminum Brazing Rods (30 pc) |
 |
Brazing Rod | High-Purity Aluminum | 13 inches | Low-temp torch brazing — thin aluminum and Al-Mg alloys |
| WISUNO E6013 3/32 Stick Electrodes (1 lb) |
 |
Stick Electrode (SMAW) | Carbon Steel | ~14 inches (1 lb pack) | Light fabrication, thin-plate repairs, beginner stick welding |
| WISUNO E6013 1/8 Stick Electrodes (1 lb) |
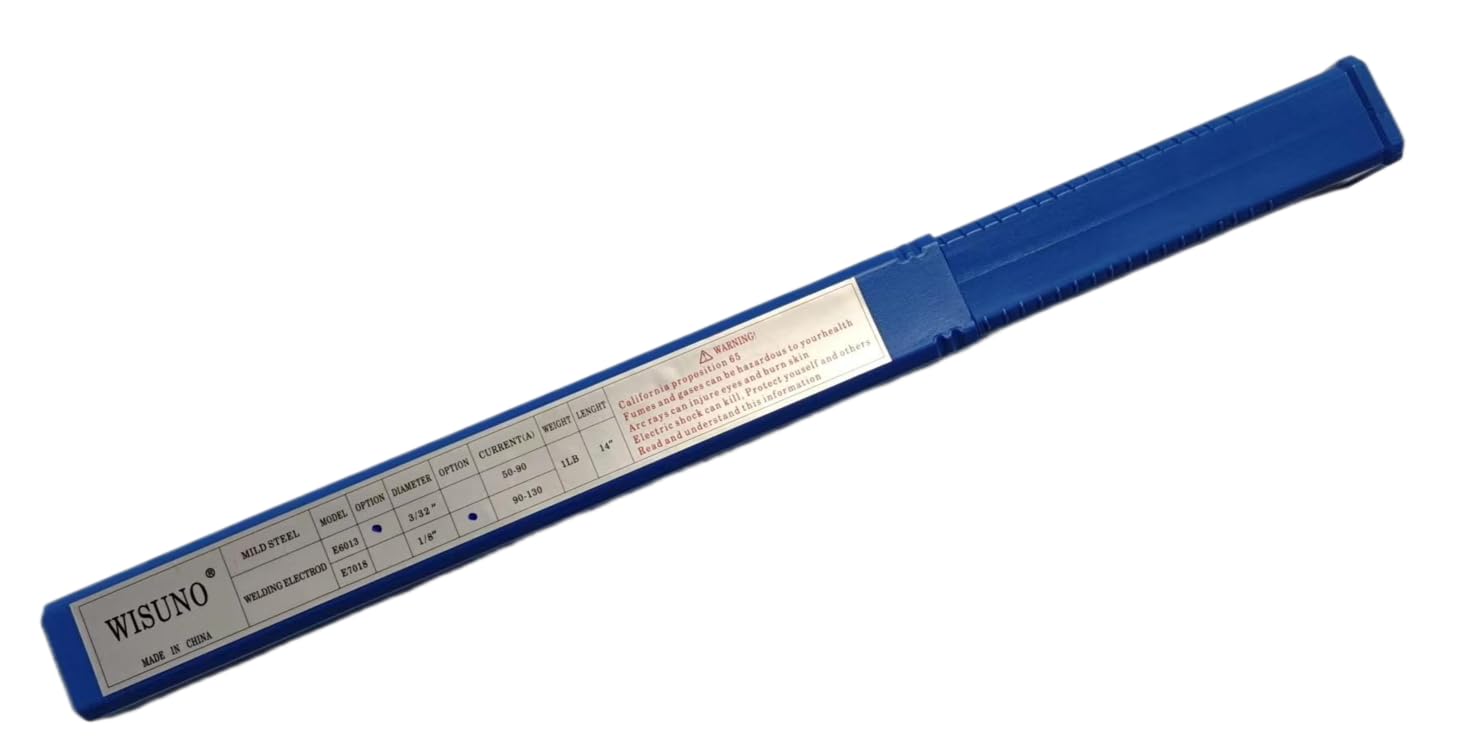 |
Stick Electrode (SMAW) | Carbon Steel | ~14 inches (1 lb pack) | Heavier mild steel repairs, farm equipment, general fabrication |
| WeldingCity ER70S-6 TIG Filler Rods (5 lb) |
 |
TIG Filler Rod (GTAW) | Mild Steel (ER70S-6) | 36 inches | TIG welding mild steel — fabrication, repair, bench work |
| AZB Flux Core Aluminum Rods (50 pc) |
 |
Flux-Core Brazing Rod | Aluminum with built-in flux | 13 inches | Torch brazing thin aluminum — patches, pontoons, small repairs |
| VITASHYNX Low-Temp Aluminum Brazing Rods (60 pc) |
 |
Brazing Rod (torch) | Aluminum with built-in flux | 13 inches | Low-temp propane/MAPP torch brazing — thin aluminum repairs |
| WISUNO E7018 Stick Electrodes (1 lb) |
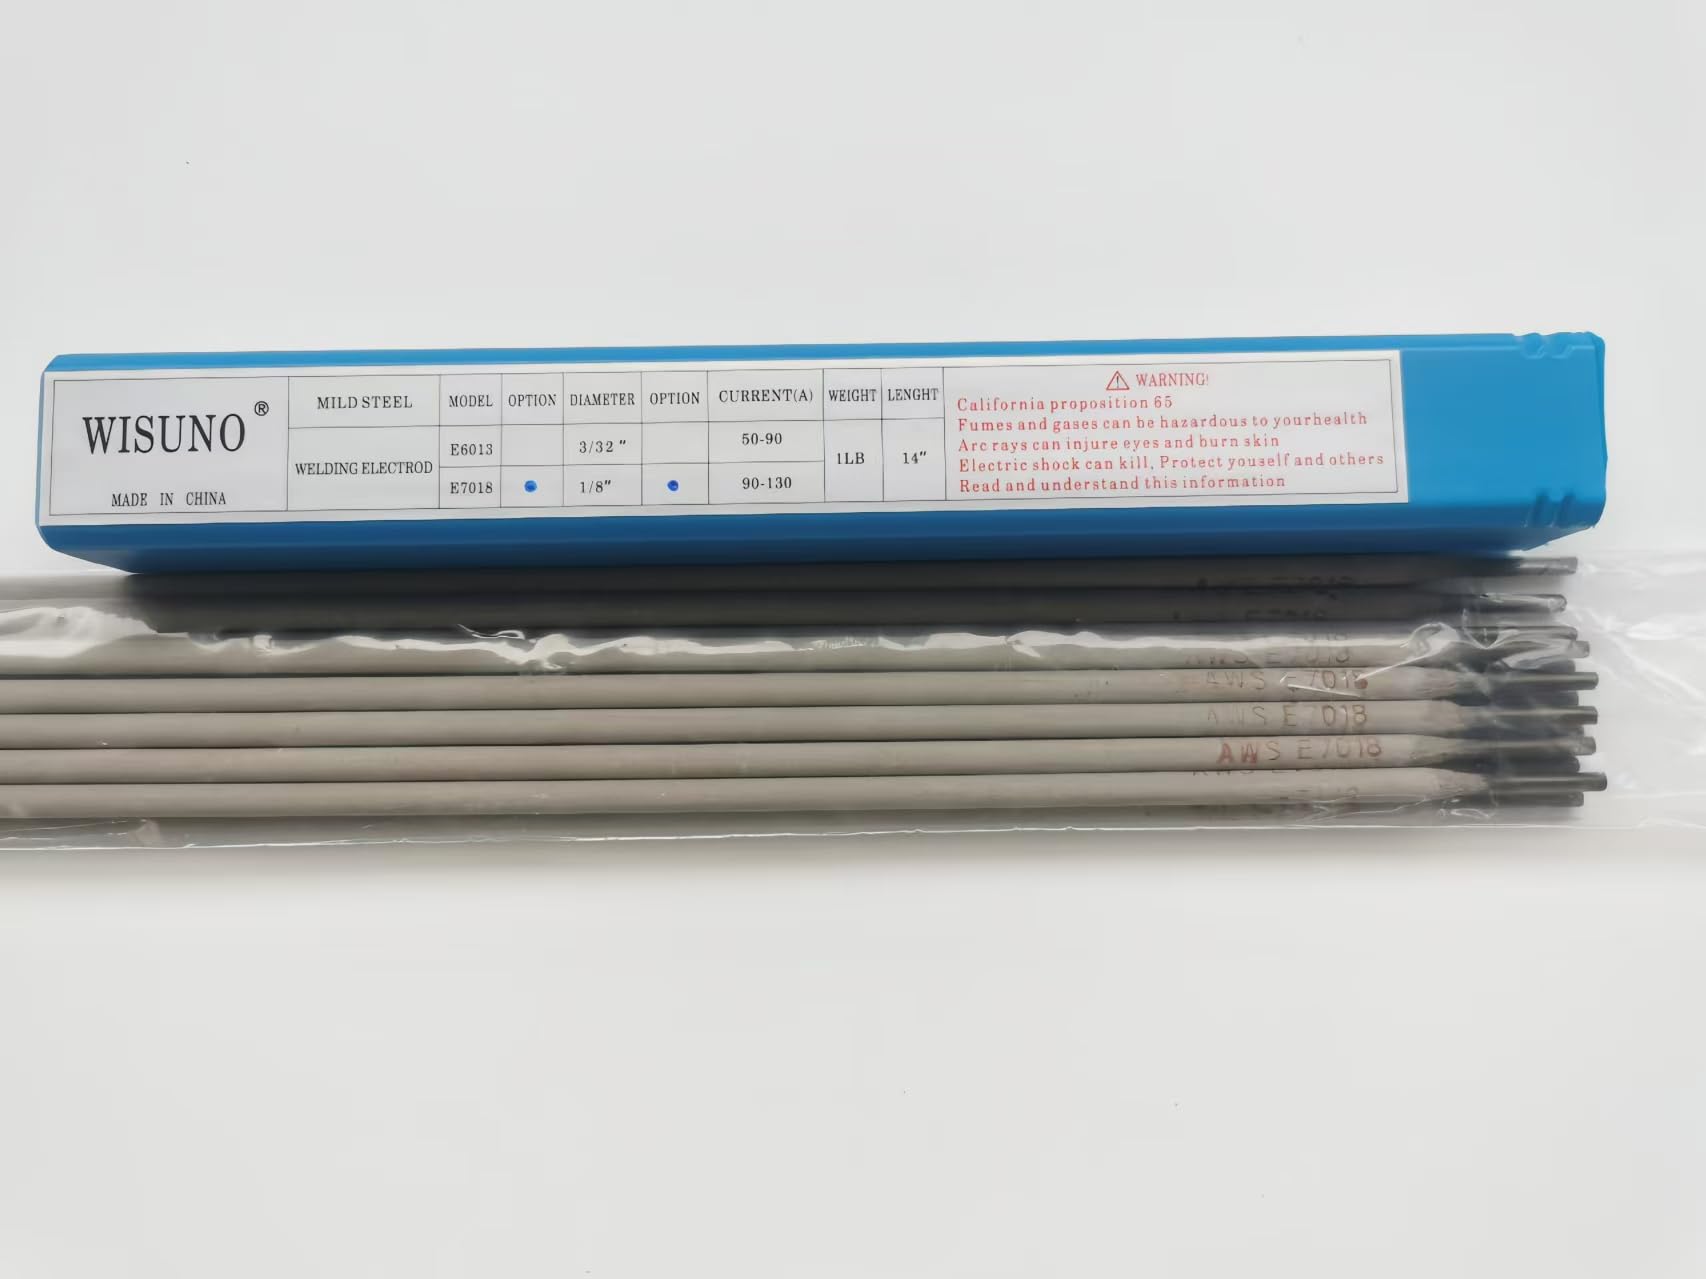 |
Stick Electrode (SMAW) | Carbon Steel, Low-Hydrogen | ~14 inches (1 lb pack) | Structural welds, load-bearing repairs, equipment fabrication |
| Convivium ER308L Stainless TIG Filler Rods (20 pc) |
 |
TIG Filler Rod (GTAW) | Low-Carbon Stainless (ER308L) | 16 inches | TIG welding 304 stainless — repair, light fab, food-grade work |
| NIEFARG Aluminum Brazing Rods (30 pc) |
 |
Brazing Rod (torch) | Aluminum | 13 inches | Torch brazing thin aluminum — experienced users only |
| Forney 42401 Supercote Hardfacing Electrodes (1 lb) |
 |
Hardfacing Electrode (SMAW) | Super Hard Facing Alloy | ~15 inches (1 lb pack) | Surface buildup, abrasion overlay — anvils, machine parts, wear plates |
Related guides: TIG welding filler rod selection chart | which welding rods need oven storage | stick welding rods compared | welding rods for stick and TIG welding
FAQ
What are the main types of welding rods?
Stick electrodes such as E6013 and E7018 carry a flux coating and run in a stick welder. TIG filler rods such as ER70S-6 and ER308L are bare wire used with a TIG torch and shielding gas. Brazing rods are melted with a torch rather than an arc, and hardfacing electrodes build up worn surfaces.
What do the numbers on an E6013 or E7018 rod mean?
E stands for electrode. The first two digits give the minimum tensile strength in thousands of psi, so 60 means 60,000 psi and 70 means 70,000 psi. The third digit is the welding position (1 means all positions), and the last digits describe the coating and current type: 13 is a rutile coating for AC or DC, and 18 is a low-hydrogen coating.
Can I use TIG filler rods in a stick welder?
No. TIG filler rods are bare wire with no flux, so they cannot sustain an arc in a stick welder. They need a TIG machine, a tungsten electrode and shielding gas. Aluminum brazing rods are not electrodes and cannot be used in any arc welding process.
Why will my aluminum brazing rods not bond?
The usual causes are too little heat, the surface oxide layer, or the wrong rod for the job. Wire-brush the joint with a stainless brush used only on aluminum, heat the base metal to the rod working temperature, and make sure your torch can reach it. Small butane torches often cannot.
How should I store welding rods?
Keep coated electrodes dry, especially low-hydrogen E7018, which should go in a rod oven or airtight container once opened. Keep TIG filler rods in a dry tube or sealed bag, and keep brazing rods clean and free of oil.
Which Rod for Which Process
Pick by process: E6013 or E7018 for stick welding, ER70S-6 or ER308L for TIG, aluminum brazing rods for torch repairs on thin aluminum, and a hardfacing electrode when you are building up worn surfaces.
Final Verdict
Ten rods, five processes. Start with the process and metal. Stick E6013 rods are the forgiving place to start, E7018 is the upgrade for load-bearing joints, ER70S-6 and ER308L cover TIG on mild steel and stainless, aluminum brazing rods suit torch repairs, and the Forney Supercote handles hardfacing.
Match the rod to your process and base metal before you consider price. Get that right and the weld follows.