Disclosure: As an Amazon Associate, we earn from qualifying purchases. If you click a link on this page and make a purchase, we may receive a small commission at no extra cost to you.
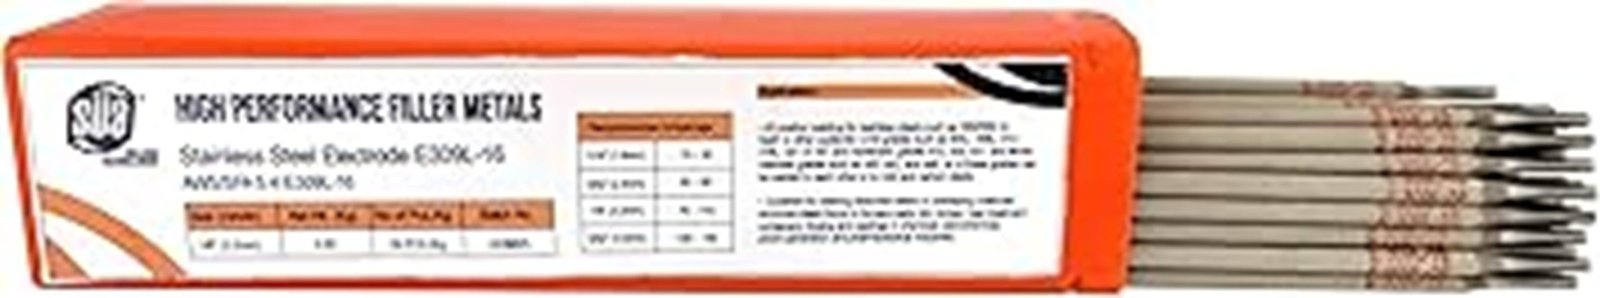
Welding stainless steel to mild steel can fail quickly if you choose the wrong electrode. The SÜA E309L-16 welding electrode is made for those mixed-metal jobs where corrosion resistance, crack resistance, and heat durability matter. It is a better fit for welders who already understand stick welding setup, amperage control, and stainless filler selection. This review explains where it performs well, where it needs care, and when a different rod makes more sense.
Quick Verdict
Rating: Recommended with caveats
Best For: Stainless-to-mild steel joints, stainless repair work, furnace parts, kiln parts, and industrial maintenance
Bottom Line: The SÜA E309L-16 is a strong pick when you need an E309L stainless stick electrode for dissimilar metals and high-heat service. It is not the easiest rod for beginners, and it is not made for aluminum or basic mild steel-only projects.
| Specification | Detail |
|---|---|
| Brand | SÜA |
| Model | E309L-16 |
| Product Type | Stainless steel stick welding electrode |
| Listing Variant Reviewed | 14″ x 1/8″ electrode, 4.4 lb package |
| Classification | AWS/SFA 5.4 E309L-16, conforms to ASME Sec. II Part C (F-5, A-8) |
| Size Options | 3/32″ and 1/8″ |
| Electrode Length | 12″ for 3/32″; 14″ for 1/8″ |
| Package Options | 0.5 lb, 2 lb, and 4.4 lb options |
| Material | Stainless steel electrode |
| Welding Current | DC+ reverse polarity recommended; AC may be used with sufficient open-circuit voltage |
| 3/32″ Amperage Range | Flat: 50 to 80 amps; vertical and overhead: 45 to 75 amps |
| 1/8″ Amperage Range | Flat: 70 to 110 amps; vertical and overhead: 65 to 105 amps |
| Tensile Strength | 86,000 psi |
| Elongation | 43% in 2″ |
| Low-Carbon Note | E309L low-carbon design; the listing references low carbon content for corrosion resistance |
| Ferrite Note | Most 309L-16 weld deposits are listed as greater than 8 FN |
| Heat Resistance | Weld deposits resist cracking and oxidation up to 2000°F |
| Compatible Metals | 309/309L, 304L, 308L, 310, 316L, 321, 347, 410, 420, 431, 430, 442, 446, and mild or carbon steels |
| Best Use | Dissimilar metal welding, stainless repair, overlay work, furnace parts, kiln linings, and industrial maintenance |
| Storage Note | Keep electrodes dry and follow the product label or shop procedure for storage and reconditioning |
What Is the SÜA E309L-16 Welding Electrode?
The SÜA E309L-16 is a stainless steel stick electrode for welding heat-resistant stainless steels and joining stainless steel to mild or carbon steel. It is not a general-purpose mild steel rod. It is a specialty stainless electrode for jobs where the weld deposit needs stronger corrosion, oxidation, and cracking resistance.
The reviewed listing is the 14″ x 1/8″ 4.4 lb version, but the same product family also includes 3/32″ rods and smaller package weights. The 3/32″ rods are 12″ long, while the 1/8″ rods are 14″ long. That gives you a choice between smaller work and heavier weld deposits.
This rod makes the most sense for welders who work on stainless fabrication, repair parts, heat-treatment equipment, kiln linings, furnace parts, or mixed-metal transitions. If you only need to weld mild steel brackets, frames, or practice coupons, a standard mild steel electrode will usually be more practical.
Key Performance Features
Stainless-to-Mild Steel Compatibility
The main reason to buy E309L-16 is dissimilar metal welding. It is designed for joining stainless grades such as 304L, 308L, 310, 316L, 321, and 347 to each other or to carbon steel. It can also work with listed martensitic and ferritic stainless grades, including 410, 420, 431, 430, 442, and 446.
That broad compatibility helps when you repair older equipment and do not always have matching base metals. It also makes the rod useful as a buffer layer when overlaying unalloyed structural steel with a stainless deposit.
Low-Carbon Deposit for Corrosion Resistance
The E309L classification uses a low-carbon design to help reduce carbide precipitation in the weld deposit. That matters most when the weld may face heat, moisture, or chemical exposure. A lower-carbon stainless deposit can help preserve corrosion resistance in the finished joint.
The listing references low carbon content in its product details. Because listing data can vary by batch or document section, treat this as a low-carbon E309L electrode and confirm exact chemistry from the product documentation when your job requires a formal weld procedure.
Higher Ferrite Content for Crack Resistance
The listing notes that most 309L-16 weld deposits are greater than 8 FN. Ferrite content helps reduce hot cracking risk in many stainless weld deposits. That is useful when you weld dissimilar steels, where thermal expansion and weld-metal chemistry can create extra stress.
This does not mean the rod can fix poor fit-up, contamination, or the wrong amperage. You still need clean base metal, correct electrode angle, controlled travel speed, and a suitable joint design.
High-Heat and Oxidation Resistance
SÜA lists the weld deposits as resistant to cracking and oxidation at temperatures up to 2000°F. That is why this rod fits furnace parts, kiln linings, heat-treatment containers, forging repairs, castings, and industrial maintenance work.
For high-heat service, the base metal, joint design, and service environment still matter. The electrode helps, but it does not replace a qualified welding procedure for code work or critical pressure, chemical, or structural applications.
Current Type and Amperage Range
The listing recommends DC+ reverse polarity. An AC machine may work when it has enough open-circuit voltage, but DC+ is the safer starting point for consistent arc behavior. This matters if you use a smaller home welder or an older AC-only machine.
For 3/32″ electrodes, the listed range is 50 to 80 amps flat and 45 to 75 amps vertical or overhead. For 1/8″ electrodes, the listed range is 70 to 110 amps flat and 65 to 105 amps vertical or overhead. Start near the low-to-middle range, then adjust after checking arc stability, slag behavior, and bead profile.
Pro Tip: Run a test bead on scrap from the same metal combination before welding the final part. It helps you confirm amperage, travel speed, slag release, and bead shape before the repair matters.
Welding Applications and Use Cases
This electrode is made for all-position welding, so you can use it on flat, vertical, and overhead work when your machine and skill level support the setup. It is especially useful when the job involves stainless steel on one side and carbon steel on the other.
- Joining stainless steel to mild or carbon steel
- Repairing stainless equipment in fabrication shops
- Overlaying unalloyed structural steels with stainless weld metal
- Repairing furnace parts, kiln linings, and heat-treatment containers
- Working on chemical, petrochemical, power generation, and pharmaceutical equipment where compatible procedures allow it
Before You Buy: This electrode is not for aluminum welding, and it is not the best first rod for a beginner learning basic mild steel stick welding. Also check the size menu carefully, because electrode count depends on diameter and package weight.
How It Performs in Real Use
For Stainless-to-Mild Steel Transitions
This is where the SÜA E309L-16 makes the strongest case. The rod is designed for stainless-to-carbon steel joints, so it gives you a better match than a mild steel rod when corrosion resistance matters. It is useful for brackets, repair transitions, and equipment modifications where stainless and carbon steel meet.
For Furnace, Kiln, and Heat-Treatment Parts
The listed resistance to cracking and oxidation up to 2000°F makes it suitable for many high-heat repair settings. It can help on furnace parts, kiln linings, heat-treatment containers, forging equipment, and castings. For critical service, follow the required welding procedure instead of relying on product claims alone.
For Repair and Overlay Work
E309L-16 can work as a buffer or overlay rod when you need stainless weld metal on unalloyed structural steel. That helps in maintenance jobs where the finished surface needs more oxidation or corrosion resistance than the base steel. Clean preparation is important because stainless electrodes do not hide contamination well.
For Shop and Field Maintenance
The all-position design helps when parts cannot be moved into a perfect flat position. In the field, the biggest risk is electrode condition. Damp rods, dirty base metal, or unstable machine output can make starts, arc control, and slag removal harder.
Setup Tips Before First Use
Start by confirming the base metals. If you know you are welding stainless to carbon steel, E309L-16 is often the right stainless stick electrode to compare first. If you are welding 304 stainless to 304 stainless, E308L may be more appropriate. If you need stronger chloride resistance, compare E316L or E309Mo-16.
Choose the rod diameter based on the material thickness and position. The 3/32″ option gives you more control on smaller work and lower amperage machines. The 1/8″ option deposits more metal and suits heavier work when your welder can run the listed amperage range.
Keep the arc tight, avoid excessive weaving, and clean slag between passes. Stainless welds can become brittle or unattractive when overheated. If the bead turns rough, undercut, or hard to control, reduce travel speed, adjust amperage, or test a different electrode angle.
Storage, Handling, and Safety Notes
Store these electrodes in a dry sealed container or rod oven according to your shop procedure. Moisture can cause unstable starts, excess spatter, poor bead appearance, and hydrogen-related concerns in some applications. Do not leave open packages exposed in a damp garage or jobsite trailer.
Use proper welding PPE, including a welding helmet with the correct shade, gloves, protective clothing, and respiratory protection when required by the material and work area. Stainless welding fumes can contain hazardous compounds, so ventilation matters. Follow the product label, safety data sheet, and local workplace safety rules.
For pressure vessels, structural jobs, chemical equipment, or regulated industrial work, do not rely on a retail listing alone. Use the approved welding procedure, qualified welder requirements, and material documentation for the job.
Who Should Buy It?
Best For
- Professional welders joining stainless steel to mild or carbon steel
- Repair technicians working on heat-exposed stainless equipment
- Fabrication shops that need an E309L-16 stainless stick electrode in common package sizes
Skip If
- You need to weld aluminum, cast aluminum, or non-steel materials
- You only weld basic mild steel and do not need stainless corrosion resistance
- You are new to stick welding and want a more forgiving practice electrode
Pros and Cons
Pros
- Designed for stainless-to-mild steel and other dissimilar steel joints
- Low-carbon E309L design supports corrosion-resistant weld deposits
- Greater-than-8-FN ferrite note helps explain its crack-resistance advantage
- Listed for all-position welding with separate amperage ranges by rod size
- Available in 3/32″ and 1/8″ sizes with 0.5 lb, 2 lb, and 4.4 lb package options
Cons
- Not suitable for aluminum welding or general non-steel repairs
- Requires dry storage and better technique than many beginner practice rods
- May be unnecessary if you only weld matching mild steel or simple 304-to-304 stainless joints
Need an E309L-16 Rod?
Check the current product size and package options before you order.
Is It Worth the Price?
The SÜA E309L-16 sits in the practical mid-range category for stainless welding consumables. It offers strong value when you need a real E309L-16 electrode for dissimilar steel work instead of a cheaper mild steel rod that does not match the job.
You get the most value if you regularly repair stainless equipment, weld stainless to carbon steel, or need rods for heat-exposed industrial parts. The available package sizes also help you avoid buying more rods than you need for smaller repair jobs.
It is not the best value if your work is limited to basic mild steel practice or simple fabrication where corrosion resistance does not matter. In that case, a standard E6013 or E7018 may cost less and feel easier to run.
How It Compares to Alternatives
Compared with E308L-16, the SÜA E309L-16 is better suited for stainless-to-mild steel joints and buffer layers. E308L usually makes more sense for common 304 stainless-to-304 stainless work. E316L is worth comparing when chloride or marine-style corrosion resistance matters more.
Compared with E309Mo-16, this E309L-16 is the simpler choice for many dissimilar steel jobs. E309Mo-16 adds molybdenum for more demanding corrosive environments. E312-16 is another problem-solver rod to compare when the base metal is unknown or crack risk is unusually high.
Frequently Asked Questions
Can the SÜA E309L-16 weld stainless steel to mild steel?
Yes. That is one of the main reasons to choose an E309L-16 electrode. It is designed for dissimilar steel welding, including stainless steel to mild or carbon steel.
What amperage should you use with this electrode?
For 3/32″ rods, the listed range is 50 to 80 amps flat and 45 to 75 amps vertical or overhead. For 1/8″ rods, the listed range is 70 to 110 amps flat and 65 to 105 amps vertical or overhead.
Can you run it on AC?
The listing recommends DC+ reverse polarity. It also states that AC may be used when the machine has sufficient open-circuit voltage, but DC+ is the better starting point for most users.
Is E309L-16 good for 304 stainless steel?
It can weld 304L and several other stainless grades, especially when joining them to carbon steel. For simple 304-to-304 stainless welding, E308L may be the more direct match.
Can it weld aluminum?
No. This is a stainless steel stick electrode, not an aluminum welding rod. Use the correct aluminum filler, process, and machine setup for aluminum work.
Does it need special storage?
Yes. Keep the rods dry in sealed storage or a rod oven when your shop procedure requires it. Moisture can hurt arc stability, bead quality, and overall weld performance.
Which size should you buy, 3/32″ or 1/8″?
Choose 3/32″ for smaller parts, thinner material, and lower amperage machines. Choose 1/8″ for heavier work when your welder can run the listed 70 to 110 amp flat-position range.
Who should skip this welding electrode?
Skip it if you only weld mild steel, need aluminum capability, or want the easiest beginner rod for practice beads. It is best for welders who need stainless corrosion resistance and dissimilar metal performance.
The Bottom Line
The SÜA E309L-16 welding electrode is a solid choice for welders who need a stainless stick rod for dissimilar steel joints, stainless repair, and high-heat maintenance work. Its main strengths are broad stainless-to-carbon steel compatibility, low-carbon E309L design, and heat-resistant weld deposits.
Skip it if you need aluminum welding, a beginner practice rod, or a simple mild steel electrode. For the right stainless or mixed-metal job, it earns a recommended-with-caveats verdict.